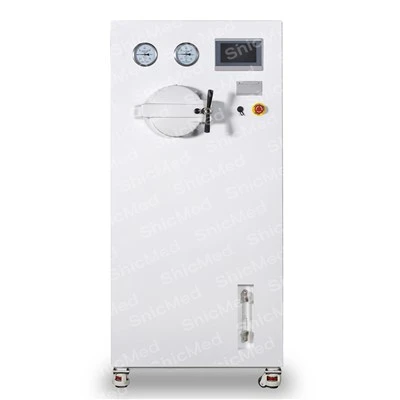
If you’ve ever stood in a pharmaceutical quality control room, watching a vial of fragile protein solution sit on a temperature probe, you understand one of the quietest, highest-stakes battles in drug manufacturing: how to make sure a life-saving medicine is completely free of harmful microbes—without destroying the active ingredients that make it work. For decades, heat sterilization was the gold standard for pharma, using saturated steam at 121°C to wipe out every last spore, bacteria, and virus. But that method was never designed for heat-sensitive drugs—think monoclonal antibodies, mRNA vaccines, insulin, or live attenuated vaccines, which lose potency, break apart, or become useless if exposed to temperatures above 80°C for even a few minutes. As a pharmaceutical sterilizer supplier, I don’t just sell equipment to manufacturers; I walk with them through the nightmare of having a batch of heat-sensitive drugs fail because sterilization wrecked the active component, delaying patient access and eating millions in R&D costs. Today, I want to pull back the curtain on how we solve this problem—not with one magic trick, but with a suite of technologies tailored to protect delicate drugs while delivering the sterility required by regulators like the FDA and EMA. Pharmaceutical Sterilizer
Let’s start with the problem, because that’s where every good solution begins. Heat-sensitive drugs are a broad category, but they share a core vulnerability: their active pharmaceutical ingredients (APIs) are often biological molecules—proteins, nucleic acids, viral vectors, or living cells—that rely on precise 3D structures to function. Heat makes those structures unravel (denature), which turns a drug that blocks cancer cell growth or prevents infection into an inert, useless powder. Even mild heat exposure, say 90°C for 10 minutes, can reduce antibody activity by 30% or more, enough to make an entire batch unfit for sale. Traditional steam sterilization? It’s non-negotiable for robust products like antibiotics, but for these delicate compounds, it’s a death sentence. So the first rule of heat-sensitive sterilization is simple: never use heat to kill microbes if you don’t have to.
That’s where the first set of technologies comes into play: non-thermal sterilization methods, built specifically for temperature-sensitive materials. Let’s talk about the most widely adopted one first, because it’s the backbone of what we supply here at our company (no fancy names, just reliable, validated solutions). It’s called Gamma Irradiation, but it’s not just blasting a drug with radiation— it’s a precision-controlled process that uses high-energy gamma rays from cobalt-60 or cesium-137 to break microbial DNA, so they can’t replicate or cause infection. The key here is that the process operates at room temperature, so the drug’s structure stays intact. But there’s a catch: not every heat-sensitive drug works with gamma. Some APIs, like certain peptides, can be damaged by direct radiation too, because the rays can break molecular bonds in the drug itself. That’s why we pair gamma irradiation with careful formulation and packaging: we work with manufacturers to choose secondary packaging that blocks excess radiation (without interfering with drug delivery) and adjust the drug’s formulation to bind the API in a way that shields it from stray rays. For example, a mRNA vaccine we helped a client sterilize last year was formulated with a sugar excipient that acted as a buffer, protecting the nucleic acid chains from radiation damage while still letting the gamma rays penetrate through the packaging to kill any residual microbes.
Another non-thermal workhorse is Ethylene Oxide (EtO) sterilization, and it’s a favorite for injectable drugs, medical devices, and even pre-filled syringes that can’t handle heat or radiation. EtO is a gaseous compound that works by alkylating microbial DNA and proteins, stopping them from growing. The best part? It runs at temperatures as low as 30°C—far below the threshold that damages most heat-sensitive APIs. But EtO has its own quirks, which is why we’ve refined our systems to address them head-on. First, EtO is toxic to humans, so our sterilizers include multiple air filtration and evacuation cycles to remove every trace of gas after the process is done, down to levels that meet FDA exposure limits (less than 1 part per million for patient use). Second, EtO can leave residual byproducts in porous materials, like the rubber stoppers used in insulin vials. That’s why we add a controlled aeration phase to our cycles, where filtered, temperature-controlled air flows through the sterilization chamber for 12 to 24 hours after EtO exposure, flushing out byproducts without raising the drug’s temperature. Last year, a client making a new GLP-1 injectable (a heat-sensitive peptide that would have failed steam sterilization) used our EtO system, and their final product had zero residual EtO levels and 98% API potency, well above their quality target.
But non-thermal methods aren’t the only answer. Sometimes, you can’t avoid using heat—you just have to make it gentler, more targeted, and shorter. That’s where our specialized moist heat systems for heat-sensitive drugs come in, designed to get the sterility assurance level (SAL) of 10^-6 (the global gold standard, meaning 1 in 1 million products have viable microbes) without cooking the drug. How? We use what’s called “low-temperature saturated steam with pressure hold cycles.” Instead of ramping up to 121°C, our systems operate at 80°C to 90°C, but we use pressurized steam to keep the water in vapor form, which is more effective at penetrating packaging and killing microbes than dry heat. The trick here is the time: we run the cycle for 1 to 2 hours, instead of 15 minutes for standard steam sterilization, because lower-temperature steam needs longer exposure to kill spores. For drugs that can handle 85°C for 90 minutes, this is a game-changer. We worked with a small biotech last year that made a heat-sensitive monoclonal antibody for multiple sclerosis; their early steam runs at 121°C cut potency by 40%, but our low-pressure, low-temp steam cycle kept potency at 95% while achieving the required SAL. The biggest challenge here is validation—every drug has a different temperature tolerance, so we work with clients to run bioburden tests and potency assays before designing a custom cycle, because a one-size-fits-all approach doesn’t work here.
Then there’s a newer technology we’ve been integrating into our systems over the past three years: High Pressure Processing (HPP), sometimes called Pascalization. HPP works by placing sealed drug vials in a chamber filled with water, then applying pressure up to 60,000 psi (about 4,000 times atmospheric pressure) to kill microbes. The amazing thing about HPP is that pressure doesn’t damage molecular structures—unlike heat, which unravels proteins, pressure compacts molecules without breaking their 3D shape. That’s why HPP is perfect for the most delicate heat-sensitive drugs, like live vaccines and cell therapies. We’ve seen clients use HPP to sterilize adenovirus vectors for gene therapies, where even a 1°C temperature spike would inactivate the virus, but HPP left the virus’s infectivity (the key to working as a therapy) at 99% of pre-sterilization levels. The only downside of HPP is that it’s less effective against bacterial spores, so it’s usually paired with a pre-treatment step—like a short gamma irradiation run—to kill spores, then HPP eliminates remaining vegetative bacteria. It’s a two-step process, but it’s far gentler than any heat method.
But here’s the part most people don’t talk about: sterilization isn’t just about the technology you use—it’s about controlling every variable along the way, because even small mistakes can ruin a heat-sensitive drug. For example, during EtO sterilization, humidity matters: if the chamber is too dry, the gas can’t penetrate microbial cell walls, so you have to add just the right amount of moisture (around 50% relative humidity) to make it work. If it’s too humid, water can get into the drug’s packaging and degrade the API. Our systems have in-line humidity sensors that adjust automatically, so clients don’t have to manually tweak settings, which reduces human error. For gamma irradiation, the dose matters: too low, and you don’t kill all microbes; too high, and you damage the API. We design custom dose maps for every client, using predictive modeling to make sure every part of the chamber gets the precise dose it needs, while the drug products stay within their safe dose range. We also include real-time data logging, which is required for regulators, so clients can prove every batch was sterilized correctly—no gaps, no guesswork.
Another critical factor is packaging. You can have the best sterilizer in the world, but if the drug’s packaging doesn’t let the sterilizing agent reach every surface, or if it leaches chemicals into the drug, the product fails. For heat-sensitive drugs, we work closely with packaging suppliers to choose materials that are compatible with our sterilization methods. For example, for EtO, we use Tyvek wrappers or breathable plastic films that let the gas pass through, but keep contaminants out after sterilization. For HPP, we use rigid, impact-resistant vials that don’t deform under pressure, and for low-temperature steam, we use autoclavable polymer packaging that won’t melt at 90°C. We even help clients run compatibility tests: exposing small samples of their packaging to our sterilization cycles, then testing for residual chemicals or API degradation, to make sure the combination works before they run full production batches.
I’ve been in this industry for 18 years, and I’ve seen hundreds of manufacturers struggle with heat-sensitive sterilization. I remember a client in 2019 that was developing a new mRNA flu vaccine. They tried gamma irradiation, but the radiation broke the mRNA strands. They tried EtO, but the residual byproducts made patients sick in early trials. They tried low-temperature steam, but the antibody stability was too low. We worked with them to combine EtO with a custom aeration cycle, and we adjusted the vaccine’s formulation to add a small amount of trehalose (a sugar that stabilizes mRNA) that protected the nucleic acid from EtO damage. Their final batches had 97% potency, zero residual gas, and passed all regulatory tests, and their vaccine launched two years ahead of their original timeline. That’s the reason I love this job: it’s not just selling equipment, it’s helping bring life-saving drugs to patients.
Now, none of this works without strict compliance. Regulators like the FDA, EMA, and WHO have very specific rules for sterility, residual byproducts, and process validation for heat-sensitive drugs. Our systems are designed and validated to meet all current GMP (Good Manufacturing Practices) requirements, and we work with clients to help them through every step of regulatory approval. That includes providing detailed process records, calibration logs, and validation reports for every sterilization cycle, so they can submit their applications without missing key data points. We also offer ongoing support: our team of application scientists works with clients for the first 10 production runs, helping them optimize cycles, troubleshoot issues, and adjust settings if their drug formulation changes.

If you’re a pharmaceutical manufacturer dealing with heat-sensitive drugs—whether it’s monoclonal antibodies, mRNA vaccines, live attenuated vaccines, cell therapies, or peptide injectables—you don’t have to settle for failed batches or delayed launches. Our range of specialized pharmaceutical sterilizers is designed exactly for this challenge, with custom cycles, real-time monitoring, and strict compliance built in. We work with you to understand your drug’s specific needs, not just sell you a one-size-fits-all machine. To discuss how we can help your heat-sensitive drug reach patients safely and on time, please reach out to our team for a procurement consultation.
Biological Indicator Evaluation Resistometer References
- Block, S. S. (2001). Disinfection, Sterilization, and Preservation (5th ed.). Lippincott Williams & Wilkins.
- Food and Drug Administration. (2023). Sterilization Process Validation and Current Good Manufacturing Practice Requirements for Sterile Drug Products. U.S. Department of Health and Human Services.
- Denyer, S. P., Stewart, G. S. A. B., & Hugo, W. B. (2004). High-Pressure Inactivation of Microorganisms. Journal of Applied Microbiology, 96(1), 19–26.
- Esposito, D., & Senkal, Y. (2019). Sterilization Technologies for Biopharmaceutical Products: A Review. Biotechnology Progress, 35(3), e2778.
- World Health Organization. (2021). Guidelines for the Sterilization of Pharmaceutical Products for Human Use. WHO Press.
Sinicmed Engineering Co., Ltd.
As one of the most professional pharmaceutical sterilizer manufacturers and suppliers in China, we’re featured by quality products and good service. Please rest assured to buy customized pharmaceutical sterilizer at competitive price from our factory. Also, quotation is available.
Address: No.251 Shangcheng, Liuquan Road, Zhangdian District, Zibo City, Shandong Province, China
E-mail: sales@sinicmedtech.com
WebSite: https://www.sinicmedtech.com/
