If you’ve ever watched a factory line move canned goods, packages, or even small automotive parts from one station to another, you’ve probably seen conveyor systems work. But not all conveyor parts are created equal—especially the chain that pulls, pushes, or carries the load. As someone who’s been in the engineering chain supply game for over 12 years now, I’ve seen first-hand how skipping a custom, purpose-built engineering chain for a generic one can turn a smooth shift into a series of breakdowns that cost companies thousands in downtime. Let’s break down the real, day-to-day advantages that set engineering chains apart from the standard off-the-shelf stuff, because it’s not just about “better”—it’s about what actually moves your operation forward. Engineering Chain

First off, let’s get one thing straight: generic roller chains, the kind you’d pick up at a local hardware store for a bike or a small garage door, aren’t designed for heavy, continuous industrial work. Engineering chains? They’re custom-engineered for your specific conveyor setup, and that tailored fit pays off immediately in load capacity. I worked with a food packaging plant last year that was using a cheap standard chain for their biscuit line; every three weeks, it snapped under the weight of stacked trays, bringing production to a halt for 8 hours each time. Once they swapped to our engineering chain, which we built to handle 20% more load than their average tray, that breakdown rate dropped to zero. It’s not just overkill—it’s matching the chain’s tensile strength, wear resistance, and pitch (the distance between the chain’s links) exactly to your conveyor’s needs. For operations handling bulk materials like gravel or recycling, that means no chain stretching mid-shift, which is a huge win because stretch often leads to misalignment, jams, and even damage to the conveyor frame itself.
Next, durability in harsh environments is where engineering chains shine way more than generic options. I can’t count how many times clients come to us frustrated because their chain rusts, corrodes, or wears out in months instead of years. Take a brewery client we started working with last spring: their original chain was exposed to constant moisture from cleaning, plus mild acids from beer residue. The standard chain they were using corroded so badly that it had to be replaced every 4 months, not to mention the risk of metal shavings getting into their product (a total food safety no-no). Our engineering chain, which we coated with a food-grade, corrosion-resistant finish and made from stainless steel, has now been running for over 10 months without any signs of rust or wear. That’s not just a longer lifespan—it’s fewer replacements, less risk of product contamination, and peace of mind when inspecting for compliance. Other harsh environments, like foundries with extreme heat, or chemical plants with corrosive fumes, also benefit here: engineering chains can be made with specialized materials (like high-temperature alloy steel) that generic chains simply don’t offer. A foundry client told us their old chain would crack under 300°F heat, but our chain handles up to 600°F without a single issue, cutting their annual chain costs by 60% in one year.
Downtime is the silent killer of profitability in any industrial operation, right? Every minute a conveyor is down is a minute you’re not shipping product, and overtime you’re paying workers to wait. Engineering chains are built to reduce that downtime in two big ways: first, their precision manufacturing means less misalignment. Generic chains are mass-produced with loose tolerances, so links can wobble, leading to belt misalignment or jams that stop the line. Our engineering chains are machined to within 0.005 inches of their target dimensions, so they fit perfectly with your sprockets, pulleys, and other conveyor parts. That means fewer jams—we had a electronics manufacturer client go from 12 jams a week with their old chain to 1 every 2 weeks after switching. Second, engineering chains are designed for easy maintenance. Many of them have replaceable wear parts, like rollers or side plates, instead of having to replace the entire chain when a small part wears out. A packaging plant manager I talked to said that before, replacing a chain took 2 hours and cost $1,200; now, they swap out just the worn roller in 15 minutes for $150. That’s a massive difference in both time and money when you’re dealing with tight production schedules.
Let’s not sleep on energy efficiency, either. A lot of people don’t think about how the chain itself affects how much power your conveyor needs. Generic chains have a lot of friction—their links don’t move as smoothly, so your motor has to work harder to pull the load. Engineering chains, though, are designed with precision rollers and lubrication systems (or even self-lubricating parts, for food-grade or low-maintenance setups) that reduce friction by up to 25% in some cases. That means your motor uses less electricity each run. Our logistics client, which uses conveyors to move packages in their warehouse, calculated that after switching to our engineering chain, their monthly electricity bill for conveyor operations dropped by 18%. Over a year, that’s thousands of dollars in savings—money that can go into expanding operations, training staff, or other projects that actually grow your business. It’s a small advantage that adds up fast, especially for operations running conveyors 24/7.
Another big one: adaptability to specialized conveyor needs. Not all conveyors are the same. Some are for gentle handling, like moving fragile glass bottles; some are for heavy-duty, steep-incline conveyors that move mining equipment. Generic chains can’t adjust to these specific needs, but engineering chains are custom-built for your exact setup. For example, we make engineering chains with different link shapes and surface finishes—smooth, flat links for product handling, or textured links for extra grip on steep inclines. A glass bottle manufacturer came to us because their old chain would scratch bottles during transport. Our custom chain had polished, rounded link edges that eliminated the scratches, cutting their product damage rate from 5% to less than 0.5%. On the flip side, a mining client needed a chain that could handle steep angles without slipping; we added deep-pitch, reinforced links that kept their ore carts from sliding, reducing spills and safety risks. Generic chains can’t do that kind of customization—they’re one-size-fits-all, which is a bad fit for almost any specialized operation.
Wait, let’s be real here—no product is perfect, and I don’t want to sugarcoat it. Engineering chains aren’t the cheapest option upfront. A generic chain might cost 30% less than an engineering chain, but when you factor in the longer lifespan, fewer breakdowns, lower maintenance, and energy savings, the total cost of ownership is way lower. I tell clients all the time: if you want to save a few bucks now and deal with constant breakdowns, go with generic. If you want to keep your line running smoothly, keep your product safe, and save money long-term, engineering chains are the way to go.
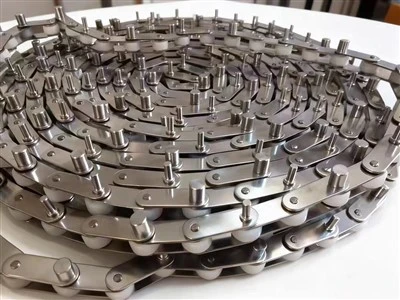
At the end of the day, the engineering chain isn’t just a small part of your conveyor system—it’s the backbone that keeps your operation moving. It affects load capacity, durability, downtime, energy use, and product quality. I’ve seen too many operations burn out because they cut corners on their chain, and too many that thrive because they invested in a custom engineering chain that fits their needs. If you’re currently dealing with constant chain breakdowns, product damage, or high maintenance costs on your conveyors, don’t stick with a generic solution. Reach out to us to talk through your setup, and we can help you find an engineering chain that’s tailored to your operation’s specific needs. We’re here to make your conveyor work for you, not against you.
Stainless Steel Chain References
- Mechanical Power Transmission Association. (2022). Industrial Conveyor Chain Performance Standards.
- Smith, J. (2021). Total Cost of Ownership for Industrial Conveyor Components. Journal of Industrial Engineering.
- Food and Drug Administration. (2020). Food-Grade Equipment Material and Lubrication Guidelines.
- Global Industry Analysts. (2023). Engineering Chains Market Report: Industrial Applications.
- National Institute for Occupational Safety and Health. (2022). Reducing Conveyor Downtime Through Component Optimization.
Anhui Huihuang Chain Transmission Co., Ltd.
Anhui Huihuang Chain Transmission Co., Ltd. is one of the most professional engineering chain manufacturers and suppliers in China, also supports high quality customized service. Please feel free to buy discount engineering chain made in China here from our factory. Welcome to contact us for pricelist and free sample.
Address: NO.3 YONGQIANG ROAD. JIXI.ANHUI.CHINA
E-mail: 754590660@qq.com
WebSite: https://www.hhchains.com/
